
CNC Cutting Tools: 12 Types, Materials and Uses
CNC cutting tools are the rotating or stationary tools that remove material on a CNC machine: drills, end mills, face mills, reamers, taps, thread mills and special cutters. The tool type decides which feature you can make; the tool material, coating and holder decide how fast and how accurately you can make it.
At Davantech we do not sell cutting tools. We use them every day in our Dongguan factory to make accurate, repeatable CNC machined parts in aluminum, stainless steel, brass and engineering plastics. This guide shows the 12 tool types we use most, how to choose a tool and coating for each material, and how tool holders affect accuracy.
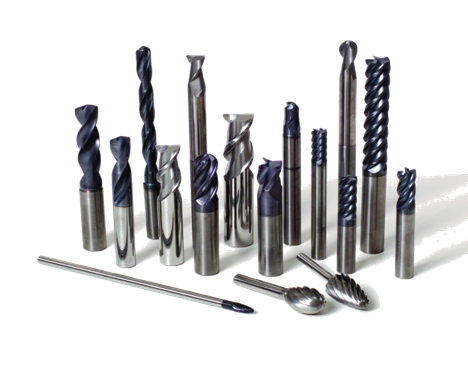
12 Types of CNC Cutting Tools
These are the cutting tools we use most to make metal and plastic parts. Knowing what each tool can do helps you design parts that are easy, and therefore cheaper, to machine.
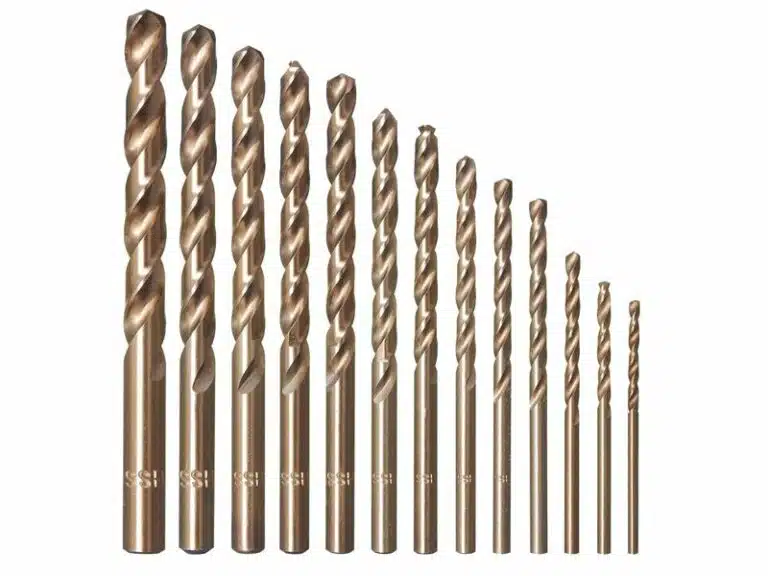
1. Drill Bits
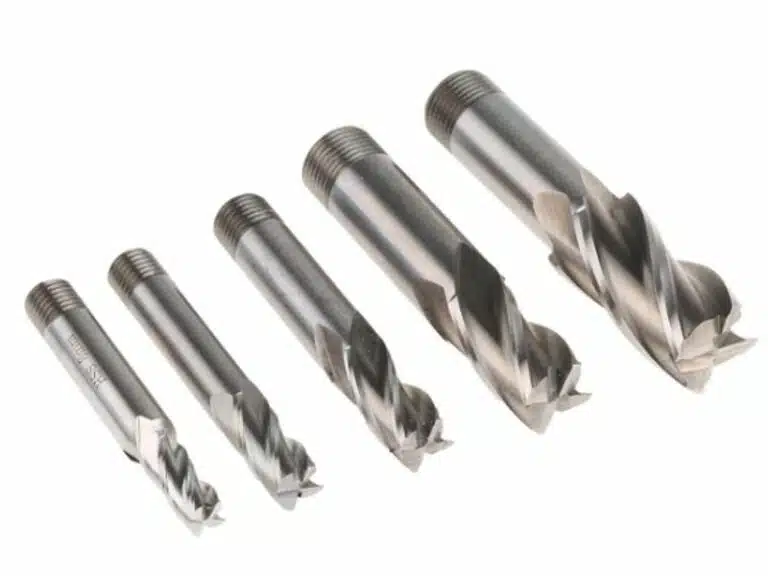
2. End Mill
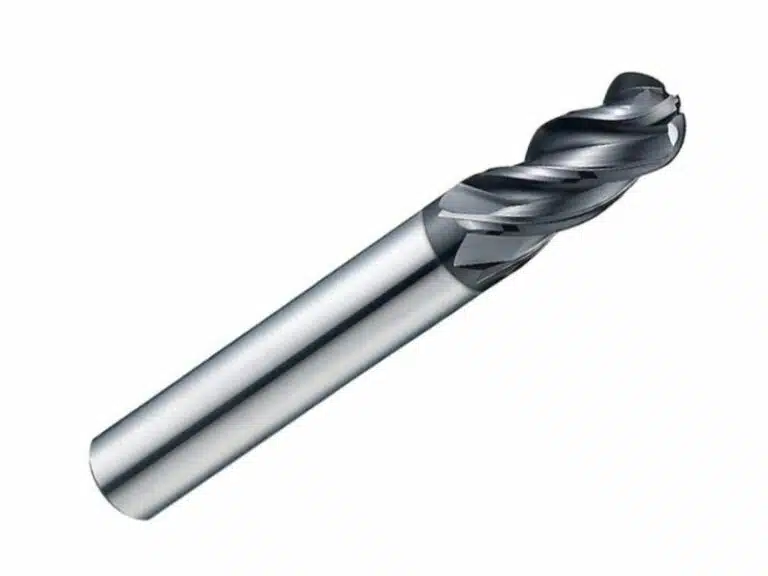
3. Ball End Mill
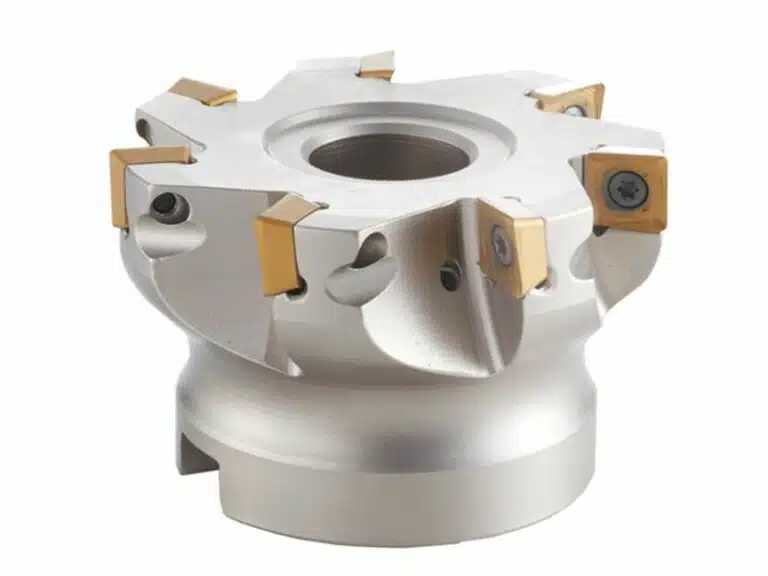
4. Face Mill
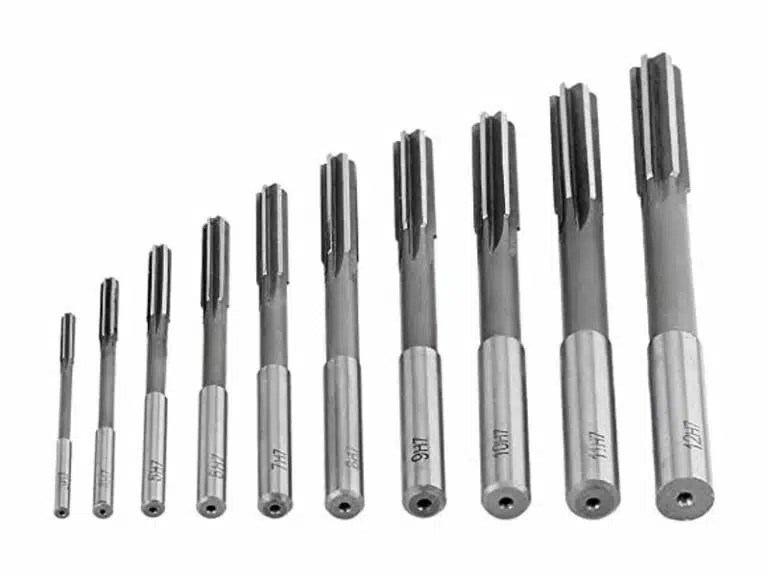
5. Reamers
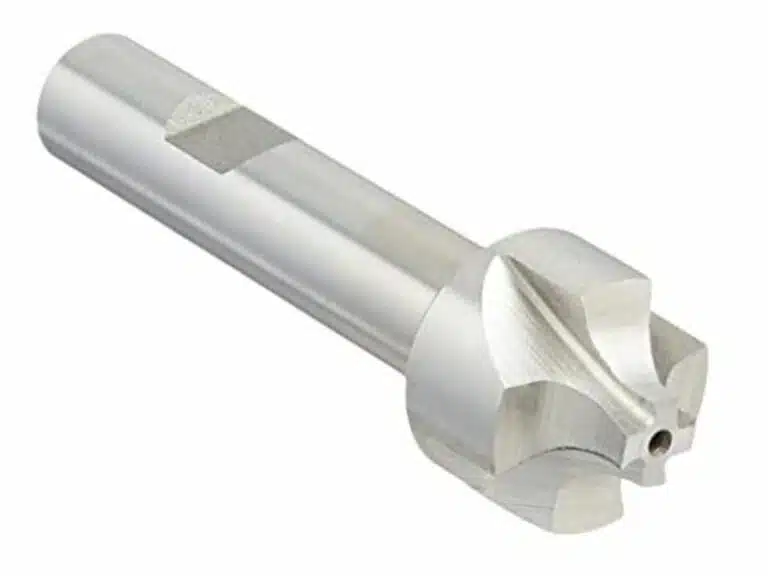
6. External Round Mill
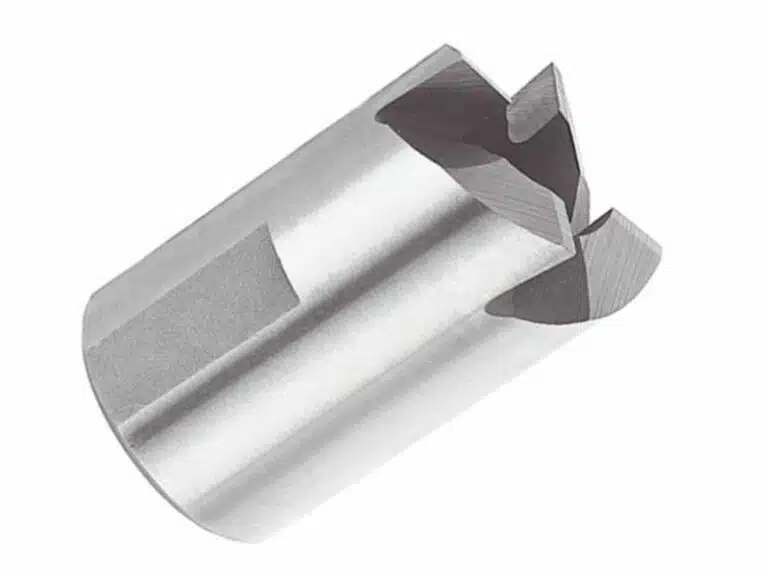
7. Hollow Mill
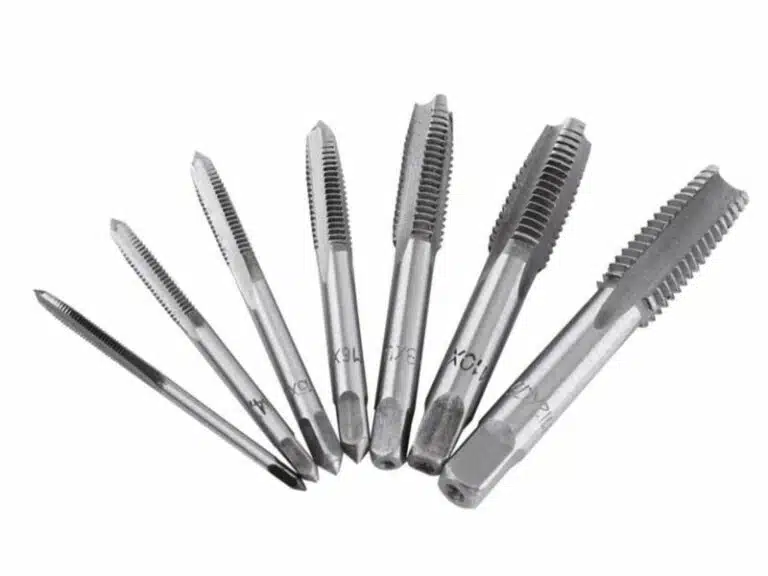
8. Thread Tap
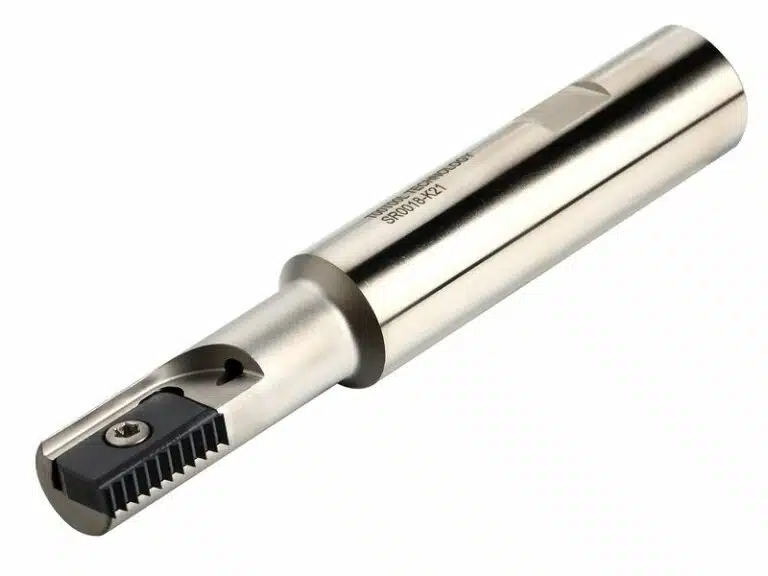
9. Thread Milling Cutter
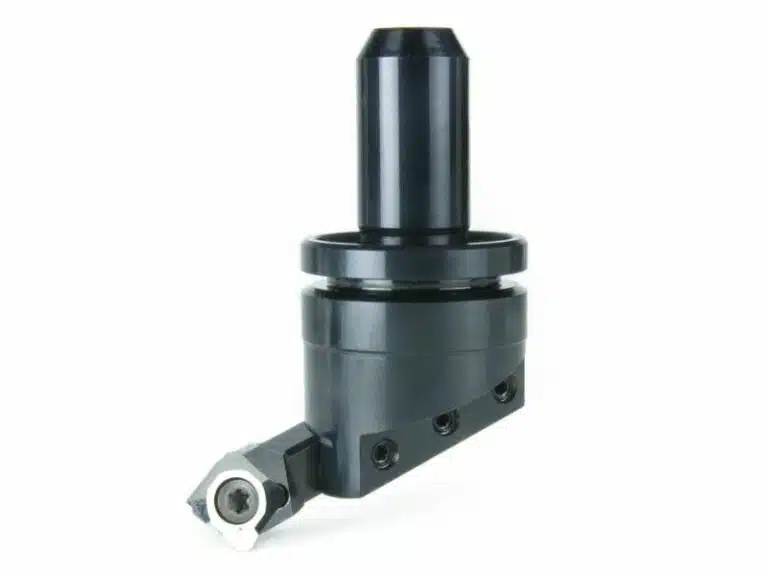
10. Fly Cutter
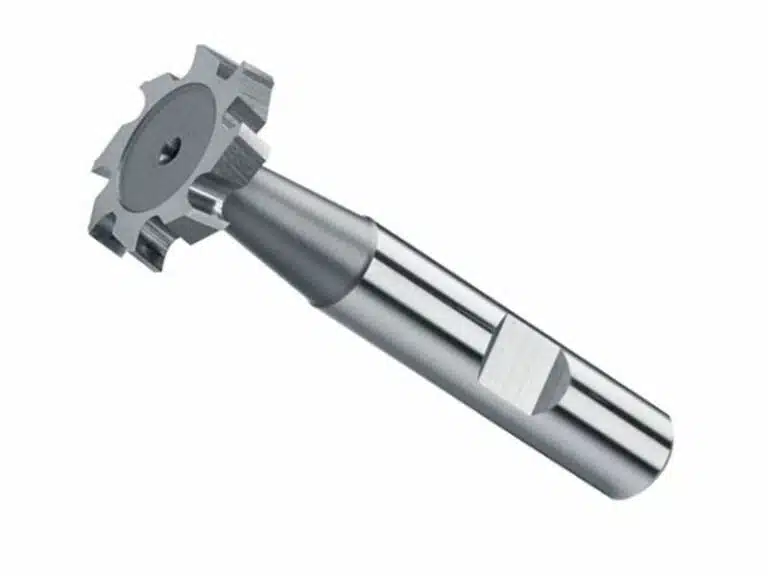
11. T-Slot Mill / Slitting Saw
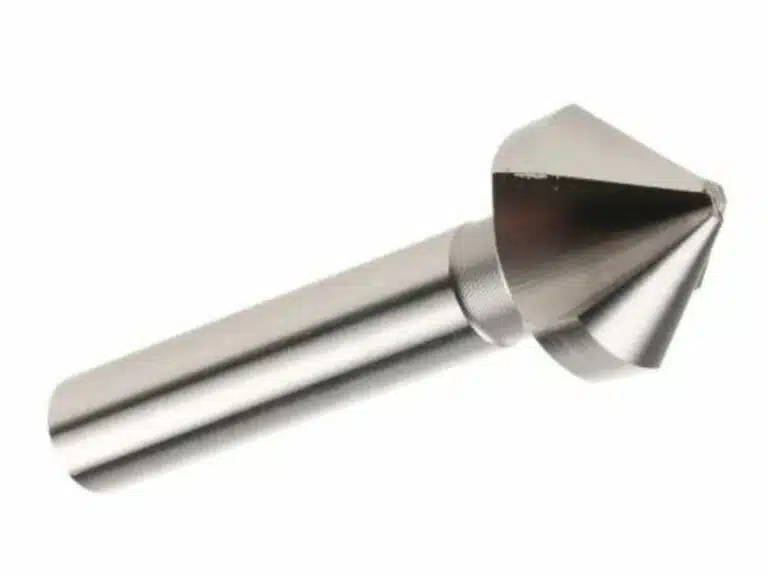
12. Countersink Mill
CNC Cutting Tools Compared: Operation, Result and Tool Material
| Cutting tool | Operation | What it produces | Typical tool material |
|---|---|---|---|
| Drill bit | Drilling | Round holes. Center drills spot the hole, twist drills drill it, ejector drills handle deep holes. | HSS or solid carbide |
| End mill | Side and face milling | Pockets, slots, profiles and contours. Roughing end mills remove stock fast before finishing. | Solid carbide or HSS |
| Ball end mill | 3D contour milling | Curved surfaces, spherical cavities and fillets, using many closely spaced passes | Solid carbide |
| Face mill | Face milling | Large flat, square surfaces. Usually the first operation on raw stock. | Steel body with indexable carbide inserts |
| Reamer | Reaming | A pre-drilled hole finished to a tight diameter tolerance and smooth bore | Solid carbide or HSS |
| External round mill | Corner rounding | A radius on external edges instead of a sharp corner | Solid carbide or HSS |
| Hollow mill | Hollow milling | A cylindrical stud or boss of set diameter, cut by plunging straight down | HSS or carbide |
| Thread tap | Tapping | Internal threads in drilled holes, for screws that mount electronics or mechanical parts | HSS or HSS-cobalt |
| Thread cutting mill | Thread milling | External threads such as those on bolts, cut by a circular toolpath | Solid carbide |
| Fly cutter | Facing | A smooth, flat surface on a rough face, cut quickly by a single tip on a long arm | Carbide or HSS cutting bit |
| T-shape mill / slitting saw | Slotting and slitting | Undercuts, T-slots and grooves at right angles to the tool axis. Slitting saws make thin, deep cuts. | HSS or carbide |
| Countersink mill | Countersinking | Conical recesses so flat-head screws sit flush, and chamfers on hole edges | HSS or carbide |
Tool material depends on the workpiece. HSS suits aluminum and brass at moderate speeds; carbide holds its edge at higher speeds and on stainless steel.
Which Cutting Tool for Which Job?
The operation decides the tool type; the workpiece material decides the flute count, the tool material and the coating. This is how we choose in practice.
| Feature to make | Tool | Aluminum | Steel and stainless | Plastics (POM, PA66, PEEK) |
|---|---|---|---|---|
| Large flat faces | Face mill or fly cutter | Sharp polished inserts, high speed | Coated carbide inserts, lower speed | Fly cutter or sharp end mill for a clean surface |
| Pockets, slots, profiles | End mill | 2 to 3 flutes, polished, uncoated or DLC | 4 or more flutes, TiAlN coated | 1 to 2 flutes, very sharp, polished |
| 3D curved surfaces | Ball end mill | Solid carbide, small step-over | Coated solid carbide | Sharp solid carbide, light cuts |
| Holes | Center drill, then twist drill | Carbide or HSS with wide flutes for chips | Coated carbide, coolant through the tool for deep holes | Sharp drill, low feed so the plastic does not melt |
| Precise holes (H7) | Drill undersize, then reamer | Carbide reamer | Carbide reamer, coated | Sharp reamer; plastic holes shrink slightly after cutting |
| Threads | Tap or thread mill | Forming tap (no chips) or cutting tap | Thread mill for large or costly parts | Cutting tap, or threaded insert for repeated assembly |
| Chamfers and countersinks | Chamfer or countersink mill | Same tool on all materials; adjust speed to the material | ||
What Cutting Tools Are Made Of
The tool material decides how hot a tool may get, and so how fast it can cut. Harder materials cut faster but are more brittle.
Cutting Tool Coatings Compared
A coating is a thin hard layer on a carbide or HSS tool. It reduces friction and heat and makes the tool last longer, but the wrong coating does more harm than good: coatings that contain aluminum react with aluminum workpieces and cause material to stick to the cutting edge.
| Coating | Color | Best for | Avoid on |
|---|---|---|---|
| Uncoated, polished carbide | Silver | Aluminum, copper, brass and plastics: the sharpest edge | Steel at high cutting speed |
| TiN (titanium nitride) | Gold | General purpose, HSS drills and taps | Hard steels at high temperature |
| TiCN (titanium carbonitride) | Blue-grey | Steel and cast iron, interrupted cuts | Aluminum |
| TiAlN / AlTiN | Violet to black | Steel, stainless steel and hardened steel, high speed or dry cutting | Aluminum |
| DLC (diamond-like carbon) | Black | Aluminum, copper, plastics and composites | Steel and stainless steel |
Tool Holders: the Part of CNC Tooling Nobody Sees
A cutting tool is only as accurate as the holder that clamps it in the spindle. If the tool runs off-center (runout), one flute does most of the cutting: the tool wears faster, the surface gets marks and holes come out oversize. Most vertical machining centers use a BT40 or SK40 taper; the holder sits between that taper and the tool.
| Holder | How it clamps | Typical runout | Used for |
|---|---|---|---|
| ER collet chuck | Slotted collet squeezed by a nut | About 0.01 to 0.02 mm, less with precision collets | General milling, drilling and tapping |
| Shrink-fit holder | Holder is heated, tool inserted, grips on cooling | About 0.003 mm | High-speed finishing, long-reach tools |
| Hydraulic chuck | Oil pressure presses a sleeve onto the shank | About 0.003 mm | Reamers and finishing, good vibration damping |
| Side-lock (Weldon) | Set screw on a flat on the shank | Higher than the others | Heavy roughing where the tool must not pull out |
| Tapping chuck | Floating holder with axial compensation | Not critical | Tapping threads |
Two habits matter as much as the holder: keep the tool stick-out as short as possible (vibration rises fast once the tool sticks out more than about 3 times its diameter), and measure every tool length before the first cut. See how we apply this in our CNC milling and CNC turning work, and how tolerances are specified in CNC machining tolerances explained.
CNC Cutting Tools Questions
How many types of cutting tools are used in CNC machining?
What is the difference between an end mill and a drill bit?
When do you use a ball end mill instead of a standard end mill?
Why is a reamer needed if a hole is already drilled?
How are internal and external threads machined?
Which tool coating is best for machining aluminum?
What materials are CNC cutting tools made from?
Does Davantech sell CNC cutting tools?
We use these tools every day to make CNC parts in aluminum, stainless steel, brass and plastics. Upload your STEP file for an instant price, or send drawings for a quote with DFM comments within 24 to 48 hours.