
Nylon CNC Machining: PA6 and PA66 Guide
Nylon (PA6 and PA66) machines well on CNC mills and lathes when the tools are sharp and the stock is dry. It cuts cleanly, wears well in service and costs less than most engineering plastics. ±0.05 mm is a starting point for drawing review; tighter critical features need individual confirmation. Agree the stock condition and inspection environment before ordering. The main risk is moisture: nylon absorbs water from the air and swells, so the size you measure on the day of machining is not always the size the part keeps.
- Machines well: bushings, spacers, gears, wear pads, insulators, rollers and housings in PA6 and PA66.
- Tolerance: define critical fits, inspection temperature and moisture condition; tighter tolerances need geometry and stock review.
- Main risk: moisture swelling. PA6 and PA66 absorb moisture and change size. Specify whether acceptance applies in a dry, conditioned or service state; drying does not prevent later swelling.

Nylon Grades for Machining
“Nylon” covers several grades that machine and behave differently. Choosing the grade is the first decision, before speeds and feeds.
| Grade | Stock | Properties | Typical parts |
|---|---|---|---|
| PA6, extruded | Rod and plate | Tough, slightly softer than PA66, absorbs more moisture | Rollers, spacers, general parts |
| PA6, cast | Large rod and plate | Available in large sections; flatness still depends on stock stress and material removal | Large wear parts, sheaves, gears |
| PA66, extruded | Rod and plate | Stiffer and more heat resistant than PA6 | Bushings, insulators, clips |
| PA66-GF30 | Rod and plate | 30% glass fibre: stiffer and abrasive to tools; directional properties need review | Structural parts, brackets; needs carbide tools |
| Oil- or MoS2-filled nylon | Rod | Self-lubricating, low friction | Bearings, slides, gears |
If low moisture uptake or tighter tolerances matter more than toughness, POM is often the better choice; see our POM machining guide and the full materials guide for CNC machining.

Nylon CNC Machining: the Process
Nylon is easy to cut but hard to keep in size. Most problems with machined PA6 and PA66 parts come from moisture, heat and internal stress, not from the cutting itself. The steps below explain the process decisions. Preparation and cutting conditions depend on the specific grade, stock thickness and geometry.
Nylon stock takes up moisture in storage. Choose drying, conditioning or stress relief to suit the agreed inspection and service state. Heavy material removal may call for roughing, stabilisation and a finishing pass.
Polished carbide end mills with 1 or 2 flutes and turning inserts with a positive rake and a chip breaker. A dull edge rubs instead of cutting, which heats the part and leaves a smeared, fuzzy surface.
Nylon melts when the tool lingers. We keep the feed high enough for a clean chip and use climb milling. If the material smears, check edge sharpness, chip evacuation and cutting heat before adjusting speed or feed.
Air helps clear chips. Where an operation needs coolant, check compatibility and its effect on moisture uptake; clean and stabilise parts before inspection. Nylon deflects under clamping pressure, so we use soft jaws, full support under thin walls and, where it fits, vacuum fixtures.
Burrs on nylon are flexible and need a sharp deburring tool or light abrasive. We measure at a stable room temperature after the part has settled, and report the measured values in the dimensional inspection report that ships with the parts.

Designing machined nylon parts
A few design choices decide whether a nylon part holds its size in service. These are the points we raise most often in our DFM review.
- Tolerance only what matters. Put ±0.05 mm or tighter on fits and bearing surfaces only. Leave the rest at ISO 2768-m. Tighter fits can add stock preparation, stabilisation and inspection time.
- Allow for swelling. A PA6 part can grow a few tenths of a millimeter over 100 mm once it absorbs moisture in use. For a bushing, send the mating shaft size, running clearance, load, temperature and humidity or water exposure. Agree the condition in which the bore is accepted.
- Keep wall thickness even. Thin walls next to thick sections warp when stress releases. Aim for walls of at least 1.5 to 2 mm and avoid long thin ribs.
- Use inserts for threads that get reused. Threads cut directly in nylon are fine for one-time assembly. For screws that are removed often, specify a threaded insert or helicoil.
- Add radii to inside corners. Sharp internal corners concentrate stress and start cracks under load. A radius of 0.5 mm or more is cheap to machine and makes the part tougher.
- Choose POM when size matters more than toughness. If the part works in a humid or wet environment and must hold tight tolerances, POM (acetal) is usually the better material. See the comparison table below.
Typical Machined Nylon Parts
Machining makes sense for nylon parts in small and medium quantities, for parts too large or thick for injection molding, and for designs that are still changing. Typical parts we machine:
- Sliding bushings, bearing sleeves and thrust washers that run with little or no lubrication.
- Wear strips, slide pads, guide rails and rollers.
- Gears, sprockets, pulleys and cam followers in low-noise, lightly lubricated drives.
- Spacers, insulating plates, standoffs and cable guides.
- Grippers, fixtures, nests and jigs that must not mark the product.
- Low volumes, before or instead of an injection mold.
For close fits in wet conditions, sustained heat or chemical exposure, review the exact grade datasheet and operating conditions. POM, PVDF or PEEK may be alternatives, but none is a universal substitute.
Cutting Parameters for PA6 and PA66
When machining PA6 (Polyamide 6) and PA66 (Polyamide 66), the recommended cutting speeds, feed rates, and other parameters depend on the operation (milling or turning) and the tool material. Below are general guidelines:
| Parameter | Turning | Milling |
|---|---|---|
| Before machining | ||
| Drying / conditioning | Use the stock supplier’s grade- and thickness-specific instructions; agree the target moisture state | |
| Annealing | Follow the stock supplier’s annealing cycle where stress relief is needed. Section thickness, heating and slow cooling determine the cycle. | |
| Cutting speed (Vc) | ||
| HSS tools | 60–180 m/min | 50–150 m/min |
| Carbide tools | 180–350 m/min | 150–300 m/min |
| Feed | ||
| Roughing | 0.1–0.3 mm/rev | 0.1–0.3 mm/tooth |
| Finishing | 0.05–0.15 mm/rev | 0.05–0.15 mm/tooth |
| Depth of cut | ||
| Roughing | 1–3 mm | 2–5 mm axial |
| Finishing | 0.2–1 mm | 0.5–2 mm axial |
| Radial engagement | n/a | Roughing up to 50% of tool diameter, finishing 10–25%, full slot up to 1× diameter |
| Tooling and cooling | ||
| Tool geometry | Positive rake 10–15°, relief 8–12°, nose radius 0.4–0.8 mm, chip breaker | Sharp, polished carbide, 1 or 2 flutes, uncoated is fine for unfilled nylon. Climb milling. |
| Coolant | Air or compatible coolant selected for the operation; account for moisture uptake and clean and stabilise before inspection. | |
Illustrative starting ranges for unfilled nylon, not a validated cutting recipe. Confirm against the stock and tool suppliers’ guidance, then trial for tool diameter, engagement and workholding. Do not transfer these ranges directly to glass-filled grades.
PA6 vs PA66 vs POM for Machined Parts
| Property | PA6 | PA66 | POM (acetal) |
|---|---|---|---|
| Moisture response | Absorbs moisture; size and properties change | Absorbs moisture; grade and condition matter | Lower uptake than nylon; check the test conditions |
| Stiffness (flexural modulus) | ~2.7 GPa | ~3.0 GPa | ~2.8 GPa |
| Melting point | ~220°C | ~260°C | ~165–175°C |
| Impact toughness | Highest | Good | Moderate, notch sensitive |
| Dimensional stability | Lowest, swells with moisture | Better than PA6 | Best of the three |
| Machinability | Good, can be gummy with stringy chips | Good, cuts cleaner than PA6 | Excellent, short chips, fine finish |
| Tolerance | Critical fits require agreed conditioning and inspection conditions | Critical fits require agreed conditioning and inspection conditions | Holds size more easily than nylon, as it absorbs little moisture |
| Pre-machining preparation | Review moisture state and stock stress | Review moisture state and stock stress | Check stock stress, temperature and material removal |
| Best for | Snap-fits, shock-absorbing parts, large structural parts, low cost | Precision parts, gears, high-load and higher-temperature parts | Small precision parts, bushings, gears and parts used in humid or wet conditions |
Typical values for unfilled grades. Check the supplier datasheet for the exact grade; glass-filled grades are stiffer and more stable but harder on tools.
Turning and Milling Nylon
Turning nylon
- Use sharp inserts with a positive, polished rake, the same type used for aluminum.
- Nylon makes long, stringy chips: use a chip breaker geometry or interrupt the feed so chips do not wrap around the part.
- Support long, thin parts with the tailstock; nylon bends away from the tool.
- Nylon expands with heat from cutting: let the part cool before the final pass and before measuring.
Milling nylon
- Use sharp 1- or 2-flute end mills with large chip space, and climb milling for a clean edge.
- Clamp firmly but without crushing; thin plates are best held on a vacuum table or in soft jaws.
- Remove material evenly from both sides of a plate to keep it flat.
- Measure parts at room temperature, and on critical parts after conditioning, because nylon takes up moisture and grows.
Need nylon molded around metal parts instead? See insert molding in PA66, or compare processes in plastic vs metal machining and plastic CNC machining vs 3D printing.
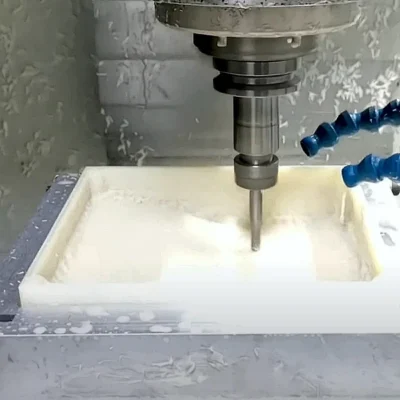
Nylon parts machined in our factory
Davantech machines PA6 and PA66 parts on its own CNC mills and lathes in Dongguan, China, from a single prototype to series production. Every order starts with a free DFM review, and every shipment includes a dimensional inspection report. The factory is ISO 9001:2015 certified and managed by a European engineering team, so you discuss drawings and tolerances in English or Dutch.
- From 1 piece
- Same process as production parts
- Design changes without tooling cost
- Drying and annealing where tolerances need it
- First article measured before the batch
- Inspection report with every shipment
- Stable process from batch to batch
- Scheduled repeat deliveries
- Option to switch to injection molding at volume
Machining or injection molding?
Machining avoids a dedicated mold and suits changing designs and smaller orders. Molding may reduce unit cost on repeat production, but the break-even quantity depends on geometry, tolerances, tooling and annual demand. Send both the first order quantity and forecast repeat quantities so the processes can be compared. See our small batch CNC machining page for how quantity affects price, or our CNC machining in China overview for the full service.
Frequently asked questions
Common questions about machining PA6 and PA66 nylon: cutting speeds, feeds, tolerances, troubleshooting and ordering, answered by Davantech's engineering team.
What are the recommended cutting speeds for machining PA6 and PA66 nylon?
What feed rates and depth of cut should I use for nylon?
Do I need to dry nylon before machining?
What coolant should I use when machining nylon?
What tolerances can I achieve when machining PA6 and PA66?
Why is my nylon part melting or smearing during machining?
Why is my nylon part warping after machining?
Should I use PA6 or PA66 for my application?
Do you offer nylon CNC machining services in China?
When is injection molding cheaper than machining nylon parts?
We machine PA6, PA66 and glass-filled nylon on our CNC mills and lathes, from one prototype to series production. Send your STEP file, drawing revision, exact grade, quantities and operating conditions. Identify critical fits and the required inspection state; a confirmed quote typically follows within 24–48 hours after complete requirements.