
Drilling vs Milling: Key Differences
Drilling makes round holes: a twist drill feeds straight into the part along its own axis, and the hole takes the diameter of the drill. Milling removes material in every direction: a rotating end mill moves in X, Y and Z to cut flat faces, pockets, slots, contours and holes of any size. On a CNC milling machine both are done in the same setup.
Below: both processes compared in one table, the difference between a drill bit and an end mill, when to drill and when to mill a hole, and how drilling and milling machines differ.
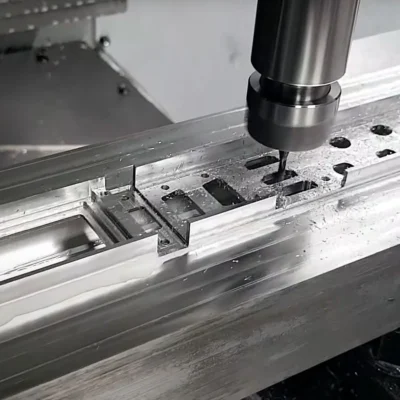
Drilling and Milling in One Table
| Factor | Drilling | Milling |
|---|---|---|
| Tool motion | Feeds along its own axis (Z) only | Moves in X, Y and Z while it rotates |
| Cutting tool | Twist drill: two cutting lips and a pointed tip (118° to 140°) | End mill or face mill: 2 to 6 flutes that cut on the side and the end |
| What it makes | Round holes | Flat faces, pockets, slots, contours, 3D shapes and holes |
| Hole diameter | Fixed by the drill size | Any diameter larger than the cutter |
| Hole bottom | Cone-shaped (drill point) | Flat |
| Typical diameter accuracy | About ±0.05 to ±0.1 mm | About ±0.01 to ±0.02 mm |
| Surface finish in the bore | Ra 3.2 to 6.3 µm | Ra 0.8 to 3.2 µm |
| Time per standard hole | Seconds | Longer: the cutter follows a circular path |
| Cost per hole | Lowest | Higher |
| Machine | Drill press, CNC mill or CNC lathe | CNC milling machine or machining center |
Typical values for CNC work in aluminum and steel. For holes tighter than a drill can hold, the hole is drilled undersize and then reamed or bored; see reaming to H7.

Drill Bit vs End Mill
The tools look alike but cut in a different way. A drill bit only cuts at its tip, so it can only go straight down. An end mill cuts on its sides as well as its end, so it can move sideways through the material.
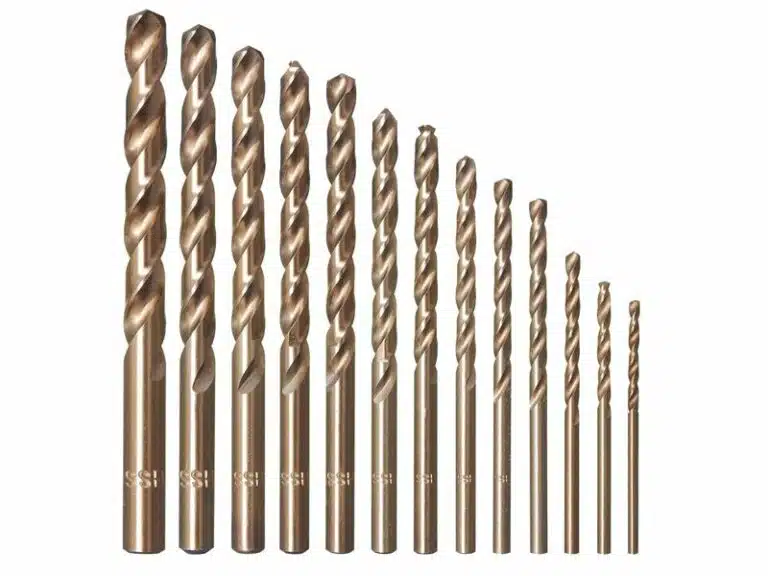
Drill bit
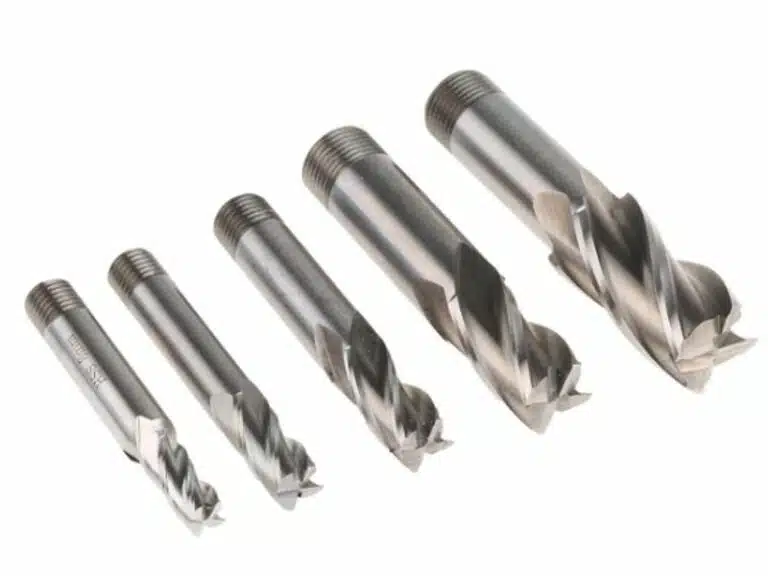
End mill
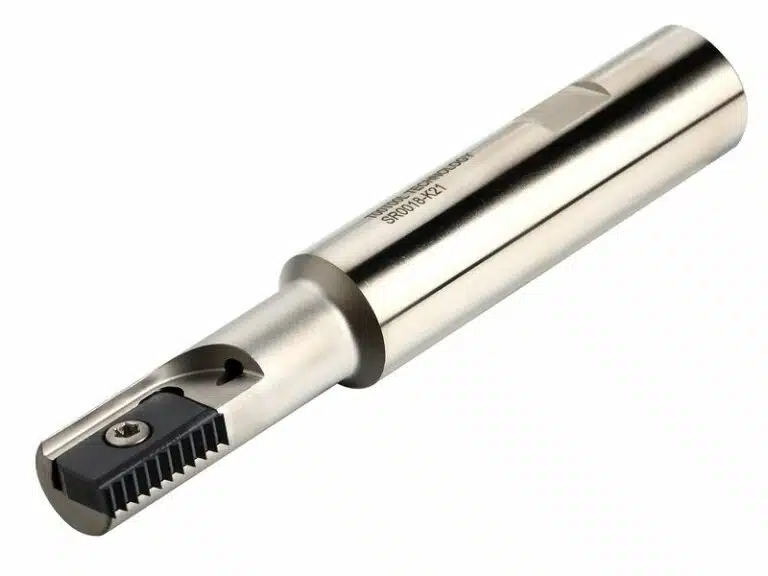
Thread mill
For all tool types, tool materials and coatings, see our guide to CNC cutting tools.
When to Drill and When to Mill a Hole
Drill the hole when
- The diameter is a standard drill size, for example for bolts, screws and dowel pins.
- A cone-shaped bottom is acceptable, or the hole goes all the way through.
- The part has many identical holes: drilling is the fastest and cheapest way to make them.
- The hole is deep: with peck drilling, holes of about 10 times the diameter are routine.
Mill the hole when
- The diameter has no standard drill, or is large enough that a drill would need high cutting force.
- The hole needs a flat bottom, a counterbore or a pocket around it.
- The hole must be accurate in size and position, or breaks through a thin wall or an existing cavity.
- One tool should make several hole sizes, to save tool changes on small batches.
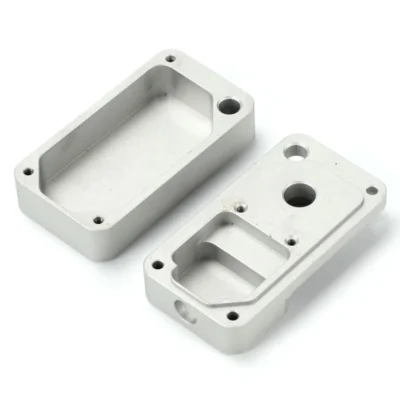
How a CNC Mill Does Both
A CNC milling machine drills with programmed drilling cycles: G81 for standard holes, G83 for deep holes with pecking, and G84 for tapping. A typical sequence is spot drill, drill, ream if the hole needs H7, tap or thread mill, and then mill the faces, pockets and contours with an end mill.
Because everything is done in one clamping, the holes stay in the right position relative to the milled features, and the part needs no second machine or setup. At Davantech this is how we make holes in milled parts, on our 3- and 4-axis machining centers. For the hole-finishing steps in detail, see drilling, reaming and tapping compared.
Drilling Machine vs Milling Machine
A drilling machine (drill press) has a spindle that only moves up and down; the operator positions the part by hand. It is simple and cheap, and suited to holes in parts that need no other machining. A combined mill-drill adds a cross table that moves, for light milling.
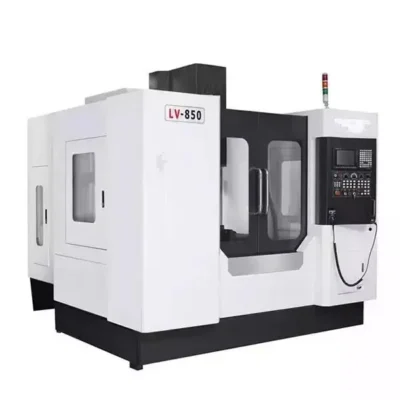
A milling machine moves the part in X and Y under a spindle that moves in Z. A CNC machining center adds an automatic tool changer, so it drills, reams, taps and mills in one program. That is why production shops make holes in milled parts on the machining center rather than on a drill press. For parts made on our machines, see CNC milling services.
Drilling vs Milling Questions
What is the main difference between drilling and milling?
Can a milling machine also drill holes?
What is the difference between a drill bit and an end mill?
Which is more accurate, drilling or milling?
When should I use drilling instead of milling?
What is the difference between a drilling machine and a milling machine?
Which process removes material faster?
Can I mill a hole instead of drilling it?
How do drilling, reaming and tapping work together?
We drill, ream, tap and mill your parts in one setup on our CNC machining centers. Send your STEP file and drawing for a quote with DFM comments within 24 to 48 hours.