
Reaming vs Drilling vs Tapping
Drilling makes the hole, reaming brings it to an exact size and finish, and tapping cuts a thread in it. This guide shows how each works on a CNC machine, what accuracy to expect and when to use which. For reamer types and tolerance tables, see What Is Reaming.
The Three Operations Compared
| Drilling | Reaming | Tapping | |
|---|---|---|---|
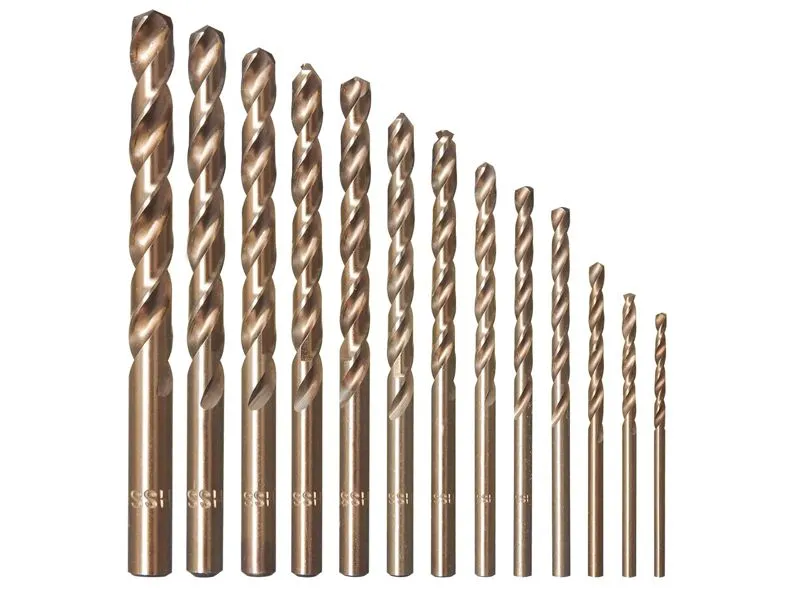 |
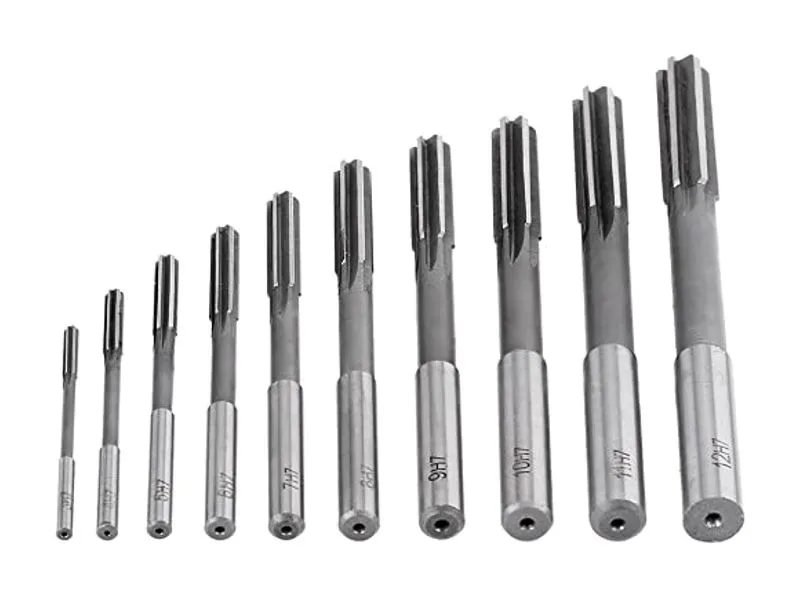 |
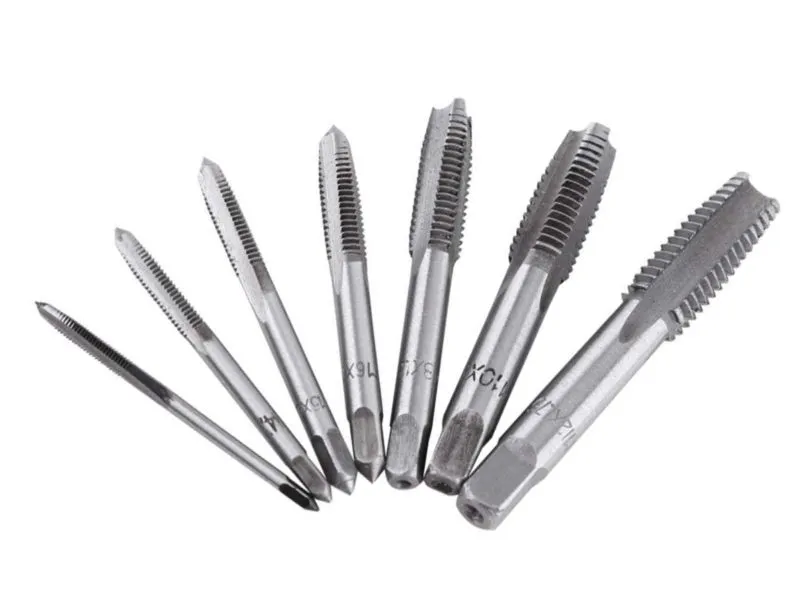 |
|
| Purpose | Make a hole in solid material | Bring a drilled hole to exact size, roundness and finish | Cut an internal thread |
| Tool | Twist drill, spot drill, centre drill | Reamer with straight or helical flutes | Tap or thread mill |
| Typical accuracy | IT10 to IT12, about ±0.05 to ±0.1 mm on small holes | IT7 (H7), for example 0 / +0.015 mm on Ø10 mm | Thread class 6H |
| Material removed | The full hole | 0.1 to 0.3 mm on the diameter | The thread profile only |
| Surface finish | Ra 3.2 to 6.3 µm | Ra 0.4 to 1.6 µm | Depends on tap and material |
| Use it for | Clearance holes and holes to be tapped | Dowel pin holes, bearing and shaft fits | Screw and bolt connections |
Values are typical for metals on CNC machines. Tell us the fit or thread class you need and we confirm it at quotation.
What Is Drilling in CNC Machining?
Drilling makes a round hole with a rotating cutting tool. It is the first step for almost every hole on a part, including holes that are reamed or tapped afterwards.
What Is Tapping in CNC Machining?
Tapping cuts an internal thread in a drilled hole, so the part can take a screw or bolt. The tap drill size sets how deep the thread is, so it is chosen with the tap.
Where Reaming Fits
Reaming takes a small, even cut from a drilled hole to reach an exact diameter, typically H7, with a smooth wall. A reamer follows the existing hole, so it improves size and finish but not position; when position matters, the hole is bored instead. Reamer types, tolerance tables and machines are covered in What Is Reaming.
A Typical Hole Sequence
Getting Holes and Threads Right
Common Problems and Fixes
| Problem | Usual cause | Fix |
|---|---|---|
| Chips packing in the hole | Deep hole, wrong flute type, too little coolant | Peck drilling, spiral flute tap for blind holes, more coolant |
| Broken taps | Tap drill too small, chips in a blind hole, misalignment | Correct tap drill, deeper drilled hole, rigid tapping or thread milling |
| Oversize or tapered holes | Part deflection, worn or run-out tool | Better support of the part, new tool, ream after drilling |
Drilling, Reaming and Tapping Questions
What is the difference between drilling, reaming and tapping?
Drilling makes a hole in solid material. Reaming takes a small cut from a drilled hole to reach an exact size, typically H7, with a smooth finish. Tapping cuts an internal thread in a drilled hole so it can take a screw or bolt.
What tolerance does a drilled hole have?
A drilled hole is typically IT10 to IT12, about ±0.05 to ±0.1 mm on small diameters. When a hole needs a tighter fit, for example for a dowel pin or bearing, it is drilled slightly undersize and then reamed to H7.
Should I ream or bore a hole?
Ream when the hole needs an exact diameter and a smooth finish and its position from drilling is good enough. Bore when the position or straightness also has to be corrected, because a reamer follows the existing hole.
Can you tap blind holes?
Yes. Blind holes are tapped with spiral flute taps or forming taps, and the hole is drilled deeper than the thread so chips and the tap end have room. For large threads or hard materials we thread mill instead.
Send us your drawing with the fits and thread classes you need. You get a price, DFM comments and a lead time from our engineers, directly from our ISO 9001:2015 certified factory in Dongguan, China.