
CNC Machining Tolerances Explained
Tolerances are the permitted variation in a dimension. In CNC machining, a tolerance tells the machinist how far a measurement may deviate from its nominal value without affecting how the part works. For example, Ø10.00 mm ±0.05 mm means the actual diameter can be anywhere between 9.95 mm and 10.05 mm and still be within spec.
Below: why tolerances matter, the types of tolerances, standard values by process, the ISO 2768 classes, what tighter tolerances cost, GD&T, and how to put tolerances on your drawing.
Why Are Tolerances Important?
Types of Tolerances in CNC Machining
Tolerances are not one-size-fits-all. Different aspects of a part need different tolerance types, each controlling a specific characteristic of the finished component.
Standard CNC Machining Tolerances
Typical tolerances by process. Use these as a baseline when you define requirements; tighter values are achievable but cost more.
| Process | Tolerance (± mm) | Tolerance (± inch) |
|---|---|---|
| CNC Milling (3-axis) | ± 0.05 – 0.1 | ± 0.002 – 0.004 |
| CNC Turning (lathe) | ± 0.02 – 0.05 | ± 0.0008 – 0.002 |
| 5-Axis CNC Milling | ± 0.02 or better | ± 0.0008 |
| EDM (Wire or Sinker) | ± 0.005 – 0.01 | ± 0.0002 – 0.0004 |
| Grinding | ± 0.002 – 0.005 | ± 0.00008 – 0.0002 |
| Laser Cutting | ± 0.1 – 0.2 | ± 0.004 – 0.008 |
| Waterjet Cutting | ± 0.1 – 0.2 | ± 0.004 – 0.008 |
| Sheet Metal Bending | ± 0.2 – 0.5 | ± 0.008 – 0.020 |
When a drawing gives no individual tolerance, the general tolerance standard ISO 2768 applies. Its classes are in the next table.
ISO 2768 Tolerance Classes f, m, c and v
ISO 2768-1 has four classes for linear dimensions without an individual tolerance: f (fine), m (medium), c (coarse) and v (very coarse). Class m is the default for most CNC machined parts and the standard we work to when a drawing does not say otherwise. Values are ± in mm.
| Nominal size (mm) | f (fine) | m (medium) | c (coarse) | v (very coarse) |
|---|---|---|---|---|
| 0.5 to 3 | ± 0.05 | ± 0.1 | ± 0.2 | n/a |
| >3 to 6 | ± 0.05 | ± 0.1 | ± 0.3 | ± 0.5 |
| >6 to 30 | ± 0.1 | ± 0.2 | ± 0.5 | ± 1.0 |
| >30 to 120 | ± 0.15 | ± 0.3 | ± 0.8 | ± 1.5 |
| >120 to 400 | ± 0.2 | ± 0.5 | ± 1.2 | ± 2.5 |
| >400 to 1000 | ± 0.3 | ± 0.8 | ± 2.0 | ± 4.0 |
| >1000 to 2000 | ± 0.5 | ± 1.2 | ± 3.0 | ± 6.0 |
| >2000 to 4000 | n/a | ± 2.0 | ± 4.0 | ± 8.0 |
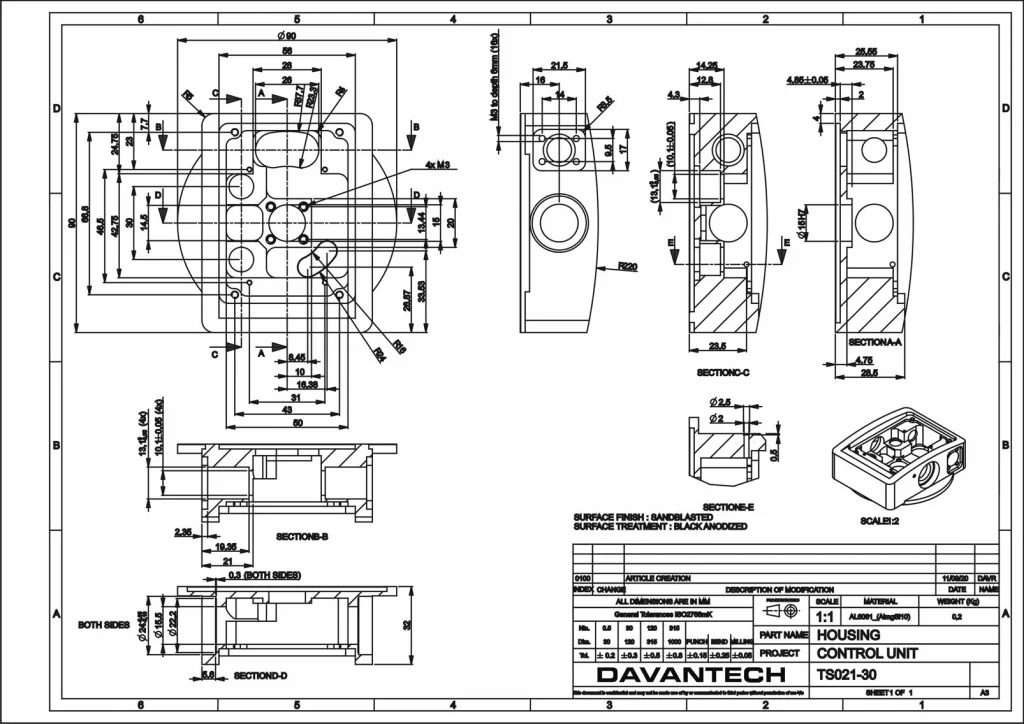
A note such as “ISO 2768-mK” combines a class from ISO 2768-1 (m, for dimensions) with a class from ISO 2768-2 (K, for geometric tolerances such as flatness, straightness and perpendicularity).
High Precision CNC Machining At Davantech
±0.005 mm
Tight tolerances achievable on precision machining runs
Dimensional Reports
Video measuring system in-house, CMM on request
Material Expertise
Aluminium, stainless steel, brass, plastics
ISO Compliance
ISO 9001:2015 quality management system
DFM Support
Engineering guidance for tolerance optimisation
What Tighter Tolerances Cost, and What Each Material Can Hold
Every step tighter means slower finishing passes, more tool changes, more measuring and more rejected parts. Tight tolerances belong on the features that need them: fits, bearing seats, sealing faces and hole positions. Everything else can stay at ISO 2768-m.
| Tolerance | What it takes | Cost impact |
|---|---|---|
| ISO 2768-m | Standard machining and sample inspection | Baseline |
| ± 0.05 mm | Careful finishing passes, more measuring | Low |
| ± 0.02 mm | Dedicated finishing tools, measuring at stable temperature | Moderate |
| ± 0.01 mm | Finishing in the same setup, critical features measured on every part | High |
| ± 0.005 mm | Selected features only, reaming or fine boring, slower cycle | Very high |
Typical tolerances by material
| Material | Practical tolerance on critical features | Why |
|---|---|---|
| Aluminum 6061, 7075 | ± 0.01 mm | Stable and easy to machine |
| Brass C360 | ± 0.01 mm | Free-cutting and very stable |
| Stainless steel 303, 304, 316 | ± 0.01 to ± 0.02 mm | Work hardening and faster tool wear |
| POM (Delrin) | ± 0.02 to ± 0.05 mm | Stable for a plastic, low moisture uptake |
| PEEK | ± 0.02 to ± 0.05 mm | Stable, but internal stresses must be relieved |
| PA66 (nylon) | ± 0.05 mm | Absorbs moisture and grows after machining |
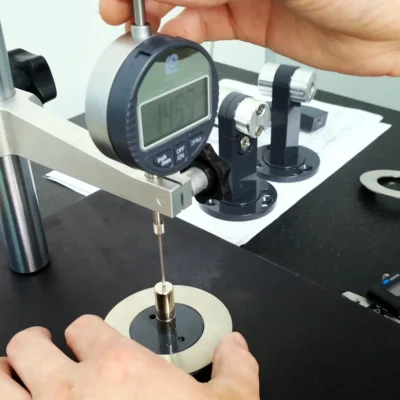
Our standard is ISO 2768-m, ±0.01 mm on critical features and ±0.005 mm on selected features, checked with calibrated hand gauges and a video measuring system. See also the POM and nylon machining guides and how to read a CNC machining drawing.
Common ISO Tolerance References
These ISO standards give tolerances a format every supplier reads the same way, which reduces ambiguity and simplifies communication.
| ISO Standard | Description |
|---|---|
| ISO 2768-m | Medium tolerance for general machining |
| ISO 2768-f | Fine tolerance, tighter than standard |
| ISO 286 IT6 | Fine grade: high-precision fits |
| ISO 286 IT9 | Coarse grade: general engineering |
| ISO 1101 | Geometric tolerancing (GD&T) |
| ISO 1302 | Surface texture / roughness indication |
GD&T: A Practical Guide
Linear tolerances control size, how long, wide, or deep a feature is. Geometric tolerances control shape, whether a surface is truly flat, whether two holes are truly parallel, whether a shaft is truly round. Both are needed to fully define a precision part. GD&T (Geometric Dimensioning and Tolerancing) is the international language for specifying these requirements, using standardised symbols defined in ISO 1101 and ASME Y14.5 so that every manufacturer reads the drawing the same way.
Controls how much a surface can deviate from a perfect plane, not its height, only its waviness. A callout of 0.05 mm means the entire surface must fit between two parallel planes 0.05 mm apart. Critical for sealing faces, base plates, and mating surfaces.
Controls how much a line or axis can deviate from a perfect straight line. Used on shafts, bores, and profiles where bowing must be limited regardless of the diameter tolerance. Prevents bowed shafts from passing a size check but failing in a bearing housing.
Controls whether two surfaces or axes are truly parallel to a reference datum. A callout of 0.02 mm means the controlled surface must lie within a zone 0.02 mm wide, parallel to the datum. Used on mating faces, guide rails, and bearing housings.
Controls whether a surface, axis, or slot is exactly 90° to a reference datum. Used on bolt hole patterns, stepped features, and any feature that must stand truly square to a base face. Without it, a hole can be within size tolerance but angled.
Controls whether the centre axis of a cylindrical feature is aligned with a reference axis. A callout of 0.03 mm means the controlled axis must lie within a cylinder 0.03 mm in diameter centred on the datum. Used on shafts with multiple diameters and rotating components where eccentricity causes vibration.
Controls the overall form of a cylindrical surface, combining roundness, straightness, and taper into a single callout. The surface must fall within two coaxial cylinders separated by the tolerance value. Used on precision bearing bores and hydraulic cylinder surfaces.
Controls the location of a feature, typically a hole, relative to datum references. Unlike a ± coordinate tolerance, true position uses a circular zone centred on the exact nominal location. More generous for assemblies, more precise where it matters. Widely used on bolt hole patterns and pin locations.
Measures total variation of a surface as a part rotates about its datum axis. Total runout combines concentricity and cylindricity. The indicator must not move more than the tolerance across the full surface during one full revolution. Used on shafts, flanges, and any rotating component.
Choosing When to Use GD&T
Specify a geometric tolerance when a linear ± tolerance alone does not fully control the functional requirement. A shaft diameter of Ø20.00 ±0.01 mm controls size, but without a straightness or runout callout, the shaft could still be bowed or eccentric and pass inspection. If the shaft drives a bearing, that matters. Add geometric callouts only where they are functionally necessary, because unnecessary GD&T increases inspection cost and supplier setup time without improving part performance.
ISO 1101 vs ASME Y14.5
Both standards use the same symbols and largely the same principles. The differences are minor but worth noting. Specify which standard applies in the title block of your drawing to avoid ambiguity.
Not sure which tolerances to specify? Share your drawing with Davantech's engineering team as part of our free DFM review. We will flag any features that are under- or over-toleranced before production begins, at no cost and no obligation.
How to Specify Tolerances on Your Drawings
To ensure clear communication and avoid delays, include the following in your technical drawings. Our engineering team can help if you are unsure.
CNC Tolerance Questions
What is the standard tolerance for CNC machining?
What tolerance can CNC machining hold?
What does ISO 2768-mK mean?
Do tighter tolerances make CNC parts more expensive?
Why do plastic parts get wider tolerances than metal parts?
How do I specify tolerances on my drawing?
We machine to ISO 2768-m as standard, ±0.01 mm on critical features and ±0.005 mm on selected features. Send your STEP file and drawing for a quote with DFM comments within 24 to 48 hours.